Case Study: CO₂ Refrigeration System for a Lincolnshire Fish Processor
Hubbard delivered an 83 kW CO₂ food processing refrigeration system for a Lincolnshire fish processor, providing efficient and reliable frozen storage.
Overview
A fish processing company in Lincolnshire appointed Hubbard to deliver a complete refrigeration solution for a new freezer cold room. The project required an energy-efficient system capable of providing reliable low-temperature performance while meeting a demanding installation programme.
Hubbard was responsible for the full design, supply and installation, including the refrigeration equipment, associated pipework and electrical components. The result was a complete CO₂ refrigeration system tailored to the requirements of a busy food processing environment.
The Challenge
Reliable frozen storage is critical within fish processing, where maintaining consistent low temperatures protects product quality and supports food safety throughout production and storage.
For this project, the customer required a new freezer cold room with sufficient capacity to meet its operational requirements. Sustainability and energy efficiency were also important considerations, with the refrigeration system needing to provide dependable performance without relying on higher GWP refrigerants.
Time was another key factor. The complete installation needed to be delivered within the customer's project programme, requiring close coordination of refrigeration, electrical and safety systems.
The Solution
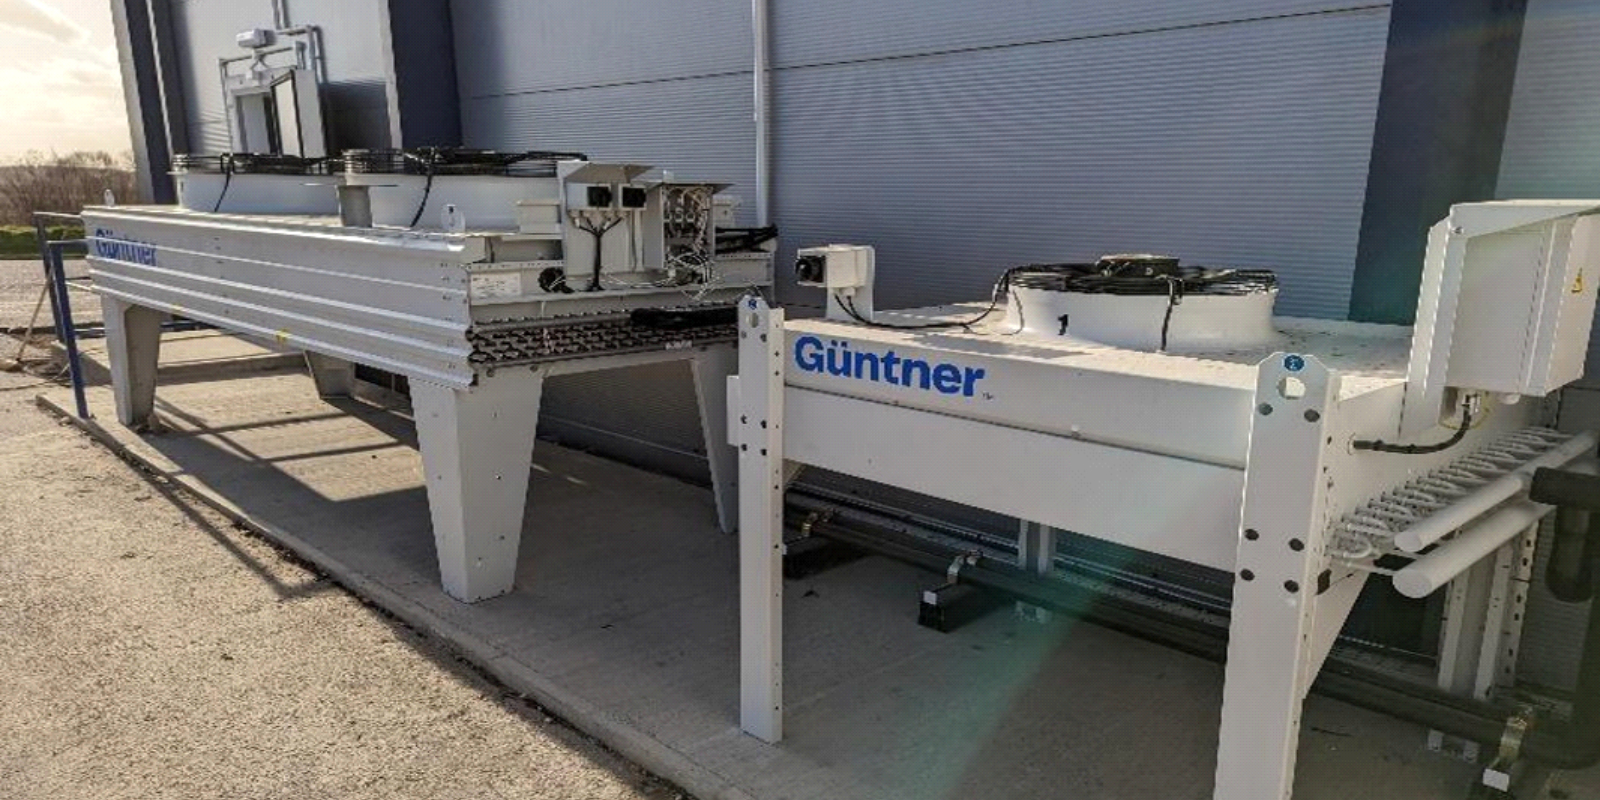
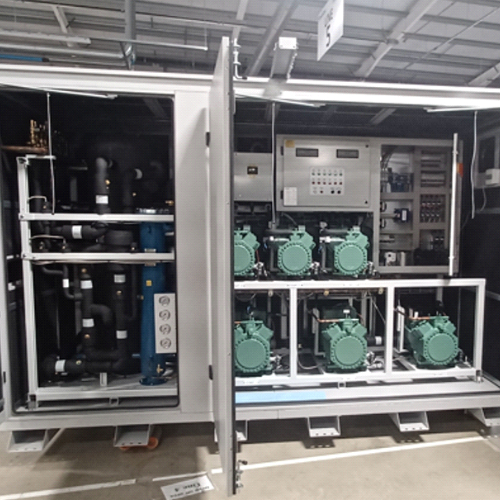
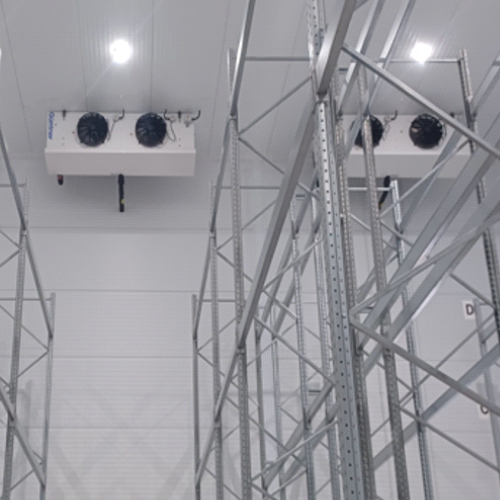
Hubbard's CO₂ specialists designed and built a transcritical booster refrigeration pack providing 83 kW duty at -30°C SST. The pack was coupled with a Güntner gas cooler and desuperheater to create an efficient low-temperature solution for the new freezer facility. Within the cold room, the system serves three Güntner ceiling-mounted evaporators.
Refrigeration services were installed within the void above the cold room ceiling using K65 copper pipework. The was pipework insulated, securely clamped and clearly labelled. Hubbard also managed the electrical elements of the installation, supplying an external distribution board and three individual control panels, one for each evaporator. The equipment was housed within weatherproof enclosures with transparent panels to provide protection while allowing straightforward visual inspection.
Safety was incorporated into the system through dedicated refrigerant leak detection. Should a leak be detected, the system alerts the customer and warns operatives not to enter the cold room until it has been inspected and cleared by a qualified engineer.
The Outcome
With refrigeration, electrical and installation expertise available within the Hubbard team, the complete project was delivered ahead of schedule and to a high installation standard. Since commissioning, the CO₂ refrigeration system has continued to perform reliably, providing the consistent low-temperature conditions required for the customer's fish processing operation. Hubbard also continues to maintain and service the installation, providing ongoing technical support and helping protect long-term performance.
Looking for a CO₂ Refrigeration System?
Whether you're developing a new food processing facility, increasing frozen storage capacity or replacing existing refrigeration equipment, Hubbard can provide a complete solution tailored to your operational requirements.
Speak to Hubbard's refrigeration specialists about your project. From initial system design through to installation, commissioning and ongoing maintenance, our team can help you specify a reliable and efficient CO₂ refrigeration system for your business.